Choosing a compressor vacuum pump is not a simple matter of comparing horsepower and price. The pump must match the required vacuum level, flow rate, gas composition, duty cycle, temperature, and maintenance environment. A compact workshop unit may struggle beside an oil mist, solvent vapor, or continuous production line. The wrong choice can create heat, noise, leaks, and avoidable downtime.
Industry data shows why efficiency deserves attention. The U.S. Department of Energy reports that compressed-air leaks can waste 20% to 30% of compressor output in poorly maintained systems. The International Energy Agency also identifies electric motor systems as a major industrial energy consumer. Vacuum equipment belongs in that discussion. Its energy demand may look modest on a product sheet, yet daily operation adds up quickly. Market research from Grand View Research estimates continued growth in the global vacuum pump market, driven by semiconductors, packaging, chemicals, and medical manufacturing. Exact figures vary between reports. That difference deserves caution.
John F. O’Hanlon, author of A User’s Guide to Vacuum Technology, emphasizes, “The vacuum system must be designed as a whole.” That principle guides this practical introduction. We will examine seven selection tips, including ultimate vacuum, pumping speed, contamination control, noise, service access, controls, and total ownership cost. Real experience matters here. A pump that reaches a perfect laboratory reading may perform poorly with a long hose, frequent cycling, or a damp process. Specifications help. They never tell the entire story.
Define the required flow before comparing pump specifications. Flow describes how quickly the pump removes air from a chamber. Manufacturers usually state it in cubic metres per hour (m³/h) or cubic feet per minute (CFM). One m³/h equals approximately 0.59 CFM. One CFM equals about 1.70 m³/h. These values describe volume, not final vacuum. A pump rated at 60 m³/h delivers roughly 35 CFM under stated test conditions, but actual performance may fall as vacuum increases.
Vacuum level needs equal attention. Check whether the specification uses absolute or gauge pressure. At sea level, atmospheric pressure is about 101.3 kPa, or 1,013 mbar. A reading of 20 kPa absolute is much deeper than 20 kPa vacuum gauge. For conversion, 1 kPa equals 10 mbar. Always record the reference clearly. Otherwise, a selection can look correct and perform poorly.
Measure the process, not only the empty vessel. Include pipe length, valve restrictions, leakage, moisture, and the time required to reach pressure. For example, a packaging chamber may need 25 m³/h at 30 kPa absolute, rather than 25 m³/h at free air. That difference matters. A common mistake is trusting a catalogue’s maximum flow without checking its performance curve. I have seen this create slow cycles and overheated motors. Real operating data is rarely perfect. Recheck it with a calibrated gauge.
Choosing a compressor vacuum pump starts with the pressure your process truly needs. Atmospheric pressure is about 1,013 mbar, while 10⁻³ mbar requires a very different system. Do not treat these values as interchangeable. Check the required vacuum, pumping speed, gas type, temperature, moisture load, and duty cycle. A pump rated near 100 mbar may suit simple suction, lifting, or packaging work. Drying, degassing, and laboratory processes may need far lower pressure. The ultimate vacuum is measured under ideal, empty, dry conditions. Real applications usually perform worse.
Look at seven practical details before purchasing. Confirm the operating pressure, not only the published ultimate vacuum. Match pumping speed to chamber volume and leak rate. Select materials that tolerate solvents, dust, or water vapor. Ask whether oil contamination is acceptable. Consider noise, heat, maintenance access, and control response. A 10⁻³ mbar target often needs staged pumping, tight seals, suitable gauges, and careful outgassing control; a basic compressor vacuum pump may not reach it reliably. I have seen users choose a powerful unit, then lose performance through a cracked hose or undersized valve. That mistake is easy to repeat. Leave safety and capacity margin, but avoid paying for extreme vacuum that the process never uses. Test the pump with the actual chamber and product, if possible. Datasheets help, but field measurements decide.
| Tip | Application or Requirement | Typical Inlet Pressure Range | Suitable Pump Technology | Key Selection Data | Important Checks |
|---|---|---|---|---|---|
| 1. Define the required vacuum level | Air movement, vacuum conveying, packaging, or simple holding | 1,013 to approximately 100 mbar absolute | Regenerative blower, side-channel blower, dry rotary vane pump, or liquid-ring pump | Required absolute pressure, free-air capacity, operating hours, and allowable noise level | Do not select a pump from gauge pressure alone; 1,013 mbar is approximate atmospheric pressure at sea level. |
| 2. Match the pump to the operating pressure | Vacuum forming, pick-and-place, woodworking, and general industrial vacuum | 100 to 1 mbar absolute | Oil-lubricated rotary vane, dry claw, dry screw, or liquid-ring pump | Pump-down time, continuous-flow capacity, ultimate pressure, and pressure stability | A pump's ultimate vacuum is measured under specified conditions and may be higher when gas ballast, leaks, vapor, or contamination is present. |
| 3. Allow for gas load and leakage | Vacuum chambers, degassing, filling, sealing, and systems with frequent door or valve cycling | 100 to 0.1 mbar absolute | Rotary vane, dry screw, dry claw, or roots booster with a backing pump | Chamber volume, leak rate, vapor load, valve conductance, and number of cycles per hour | Pump capacity at the working pressure is more useful than the nominal capacity at atmospheric pressure. |
| 4. Select oil-free equipment when contamination matters | Food packaging, pharmaceutical processing, electronics, laboratory work, and clean handling | 1,013 to approximately 0.1 mbar absolute | Dry diaphragm, dry claw, dry scroll, or dry screw pump | Oil-free gas path, particle generation, exhaust filtration, chemical resistance, and cleanability | Oil-free does not automatically mean chemically inert; confirm compatibility with solvents, acids, moisture, and process vapors. |
| 5. Handle moisture and condensable vapors correctly | Drying, evaporation, freeze-drying support, humid gas extraction, and liquid-loaded processes | 1,013 to approximately 1 mbar absolute | Liquid-ring, chemical-duty diaphragm, dry screw, or rotary vane pump with gas ballast | Vapor composition, inlet temperature, condensate quantity, water-vapor tolerance, and separator requirements | Use condensate traps, knock-out pots, separators, or gas ballast where appropriate; otherwise oil and pump components may be damaged. |
| 6. Use a multi-stage system for high vacuum | Vacuum coating, mass spectrometry preparation, electron-beam equipment, and high-vacuum research | 1 to 0.001 mbar absolute | Rotary vane or dry screw backing pump plus roots, turbomolecular, or diffusion high-vacuum pump | Required base pressure, gas load, compression ratio, pump-down time, and backing pressure limit | High-vacuum pumps generally require a backing pump and suitable isolation, venting, and protection procedures. |
| 7. Compare total operating cost and service needs | Continuous-duty production, automated systems, and installations where downtime is costly | Application-dependent: 1,013 to 0.001 mbar absolute | Technology selected according to pressure, gas composition, duty cycle, and contamination risk | Power consumption, maintenance intervals, consumables, heat rejection, spare parts, noise, and expected service life | Evaluate life-cycle cost rather than purchase price alone; oversizing can increase energy use and may reduce control efficiency. |
Reference note: Pressure values are approximate absolute-pressure ranges. Actual performance depends on temperature, gas composition, altitude, leakage, vapor load, piping conductance, and pump condition.
Begin with the required pressure.
Tip one: distinguish absolute pressure from gauge pressure. A vacuum reading of 100 mbar absolute is not the same as negative 100 kPa gauge.
Tip two: check pumping speed at the target pressure, not only the headline rating. ISO 21360-1 provides standardized methods for measuring vacuum-pump performance. Its approach reminds buyers to compare test conditions carefully. Figures can look impressive.
Tip three: match the duty cycle to real operation. Intermittent use and continuous production need different thermal designs.
Tip four: review motor power, starting current, cooling, and overload protection. More horsepower does not automatically deliver deeper vacuum.
Tip five: confirm 50/60 Hz compatibility, voltage, rotation speed, and allowable frequency variation. IEC 60034-1 treats frequency and voltage as important motor rating conditions. A frequency mismatch may increase heat, noise, or wear. I have seen a pump selected correctly on paper but poorly ventilated in practice.
Tip six: examine flow losses, hose diameter, filter restriction, and oil or moisture exposure. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that compressed air can consume about 10% of industrial electricity. It also notes that leaks may waste 20–30% of compressor output.
Tip seven: request performance curves, sound data, service intervals, and test conditions. A neat spreadsheet can still mislead. Check the numbers at your actual altitude, temperature, pressure, and operating schedule.
Choosing a compressor vacuum pump requires more than comparing pressure, flow, or purchase price. The air quality specification should guide the decision. ISO 8573-1 classifies compressed air by particles, water, and oil. Check the required class for your process before selecting oil-free or lubricated technology.
Tip 1: Identify contamination risks. Oil-free pumps reduce lubricant transfer, but they still need clean intake air, suitable seals, and regular inspection. They are often appropriate for laboratory work, packaging, electronics, and processes touching sensitive materials. However, “oil-free” does not automatically mean contaminant-free. Measure the process.
Tip 2: Consider a lubricated pump when long operating hours, high loads, or lower ownership costs matter. With correctly sized filters, separators, drains, and maintenance intervals, it may achieve the required ISO 8573-1 class. Filter performance must match the target class, not merely the pump’s advertised capacity. Small details matter.
Tip 3: Verify performance at the actual duty cycle. Record vacuum level, temperature, condensate, filter pressure drop, and service frequency. In field inspections, neglected drains often create more trouble than the pump itself. I would also allow safety margin, although excessive margin can waste energy. Ask for independent test data or documented measurements under comparable conditions. Recheck the specification after installation, because clean air at the outlet can still degrade through dirty piping, worn seals, or poorly maintained downstream equipment.
Choosing a compressor vacuum pump requires more than checking the lowest vacuum rating. Use seven practical checks: noise, energy use, maintenance, safety, duty cycle, documentation, and compliance.
Measure noise at one meter during normal operation. A quiet pump protects communication and reduces operator fatigue. Ask for tested dB values, not vague claims. Compare energy consumption at your actual working pressure. A large motor may seem powerful, but it can waste electricity during light-duty cycles. Calculate annual operating costs. Small differences become expensive.
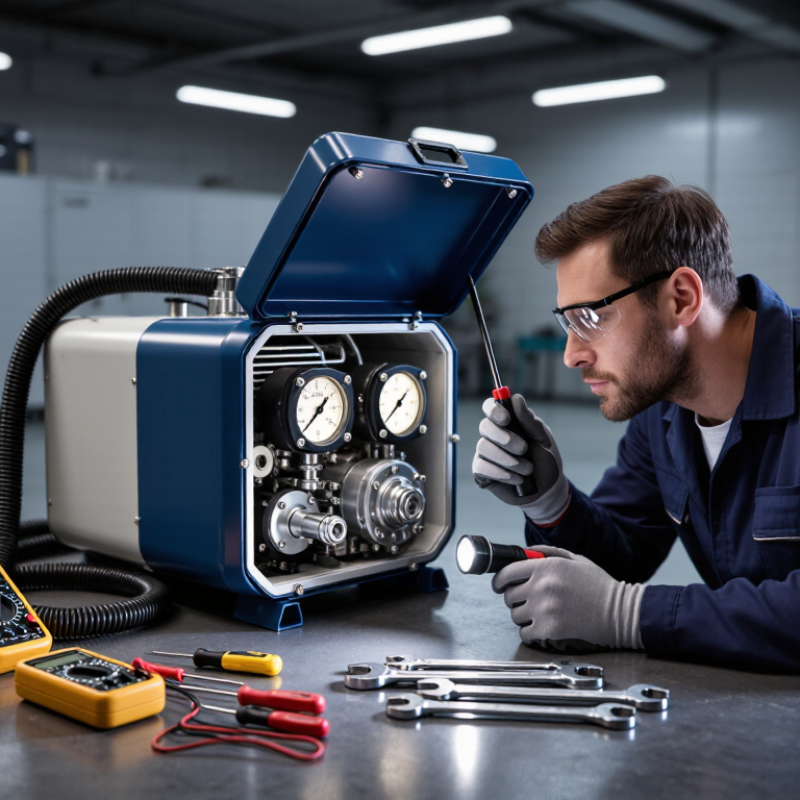
Maintenance access matters every week. Check oil filling points, filters, seals, and drain valves. I have seen equipment perform well but lose time because service panels were difficult to reach. Choose replaceable parts with clear service intervals. Safety features should include thermal protection, pressure relief, proper grounding, guards, and an accessible emergency stop. Do not assume a familiar design is automatically safe.
For CE or UL compliance, request the declaration, applicable test reports, and traceable technical files. CE marking relates to applicable European requirements, while UL evaluation depends on the specific product and standard. Ask what was actually tested. Verify voltage, frequency, enclosure protection, and installation conditions. A certificate alone does not guarantee suitability. My own mistake was trusting paperwork before checking the working environment. Temperature, dust, and continuous operation changed the decision. Leave a realistic performance margin. Content from current standards and qualified technicians should guide the final selection.